
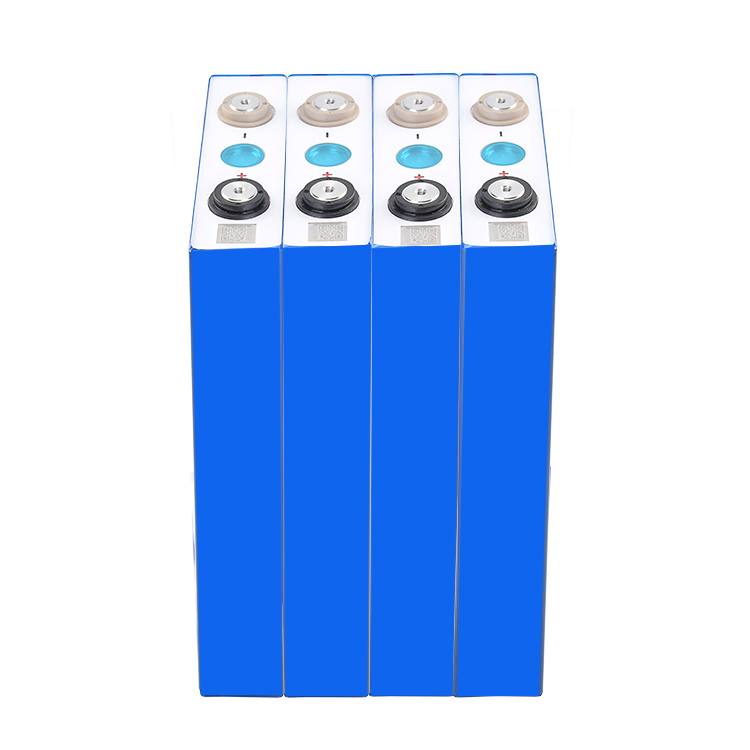
18650 lithium battery pack production process (1) Bake for 12 hours at a constant temperature and a vacuum of -0.09MPa. The main purpose is to dry out the moisture in the battery core. (2) Liquid injection: Inject the electrolyte into the vacuum-baked battery core in a glove box filled with Ar gas. The amount of liquid injected is based on the lithium battery pack setting.
18650 lithium-ion battery pack production process
(1)Baking
Bake for 12 hours at a constant temperature and vacuum of -0.09MPa. The main purpose is to dry out the moisture in the battery core.
(2)Injection
Inject electrolyte into the vacuum-baked battery core in a glove box filled with Ar gas. The amount of liquid injected varies according to the design of the lithium-ion battery pack. The battery must be weighed before and after injection. The weight difference is the amount of liquid injected. Use this to determine whether the injection volume is appropriate.
(3) Welding electrode tabs Weld the positive electrode tab (aluminum bar) and the negative electrode tab (nickel bar) to the scraper positions of the positive and negative electrode sheets using an ultrasonic welding machine. Pay attention to prevent welding deviation, welding misalignment, and false welding.
(4) Bottom welding. First put the insulating gasket into the steel case, then put the wound battery core into the steel case, and use a spot welder to weld the negative electrode lug to the bottom of the steel case. Check the outer surface of the bottom of the steel shell to find out the 18650 lithium-ion battery packs with weak spot welding such as yellow spots, black spots, defects, and fire.
(5)Sealing
First use a spot welder to spot weld the steel shell and cap of the 18650 lithium-ion battery pack, and then use a laser welder to continue laser welding. Laser welding should ensure accurate positioning and clean parts to be welded. It is strictly forbidden to cause deformation or damage to the battery. Post-welding inspections should be carried out to repair welding of defective batteries with welding holes, explosions, etc.
(6) Winding
Place the ion exchange membrane flushly on the winding needle, and the front end extends out of the winding needle by 2-5mm. There should be no wrinkles in the four corners of the pole piece. The pole piece should not fall off, the tape should be applied at an angle, the single-sided tape is too long, and the double-sided tape should not be Defects such as the left and right misalignment of the tape, the tape not covering the solder joints, etc. The positive electrode material must hug the negative electrode material, the pole piece cannot be rolled sideways, and the front end of the pole piece must be inserted to the top.

Popular recommendation
What should be paid attention to when assembling lithium batteries
2022-11-04AAA NiMH batteries.Principle and technology of nickel-cadmium battery
2023-10-09Where does the battery come from the electrical
2022-06-18button battery cr1620.How to distinguish between energy storage lithium batteries and power lithium
2023-10-10801752 lipo battery.New breakthroughs in thermal instability research: BAK Battery deeply explores h
2023-10-09no 5 alkaline battery!Breakthrough domestic technology for lithium battery separators
2023-10-08502030 lipo battery.Charging method based on high-voltage lithium-ion battery pack
2023-10-08AG Coin battery application
2022-06-18AG Coin battery
2022-06-18CR927 battery.Analyze whether OEMs should enter the lithium-ion battery industry from the four dimen
2023-10-08The Challenge of Rechargeable Batteries
2022-11-14LR521 battery!How to solve the protection obstacles of 3842 circuit
2023-10-08 EN
 CN